Reviewed by: Michael Ishlove, Technical Manager
Last reviewed: August 2026
Every industrial electric motor is specified against the conditions it is expected to see on day one. The problem is that plant environments rarely stay static, and an enclosure decision that made sense at commissioning can quietly become a liability years later. For engineers responsible for uptime, the enclosure rating on a motor nameplate is not a formality; it is the single design choice that determines whether dust, moisture and airborne contaminants reach the windings and bearings at all.
Totally Enclosed Fan Cooled (TEFC) and Open Drip Proof (ODP) motors handle that exposure very differently, and the gap between them widens the longer an industrial electric motor runs in conditions it was never designed for. This article walks through why enclosure mismatch is so easy to miss, what it actually looks like on the floor and how to build a re-evaluation step into your spec review process before the next failure forces the decision for you.
Enclosure mismatch rarely shows up as the stated cause of failure because the bearing or winding is what actually fails, not the enclosure itself. Reliability investigations that stop at the failed component instead of the operating conditions around it consistently miss enclosure exposure as the root cause.
Industry failure surveys compiled under IEEE Std 493 (the IEEE Gold Book) and corroborated by EPRI's utility motor studies attribute roughly 40 to 50 percent of induction motor failures to bearing damage, with contamination and lubrication breakdown identified as leading root causes rather than the bearing itself. Stopping a failure investigation at "the bearing failed," rather than tracing the contamination pathway back to the enclosure, is exactly how the same failure repeats itself on the next industrial electric motor.
This is precisely why enclosure mismatch stays under-diagnosed: the failure ticket says bearing, the replacement part is a bearing and the enclosure that let the contamination in keeps running unquestioned. Motor design reviews that only look backward at what broke, rather than forward at what is exposing the replacement to the same conditions, repeat the cycle indefinitely.
An ODP motor operating outside its intended clean, dry environment tends to show a specific, recognizable pattern of wear rather than a single sudden fault. Because ODP enclosures rely on open ventilation slots for cooling airflow through the windings, those same openings are the entry point for whatever is in the surrounding air.
Watch for these signatures during routine inspection or teardown, listed in the order they most reliably appear when an enclosure has become wrong for its environment:
None of these signs individually proves an enclosure mismatch. Taken together and compared against an actual environment rather than its original electric motor spec sheet, they build a strong case for re-evaluating whether TEFC protection is now the better fit.
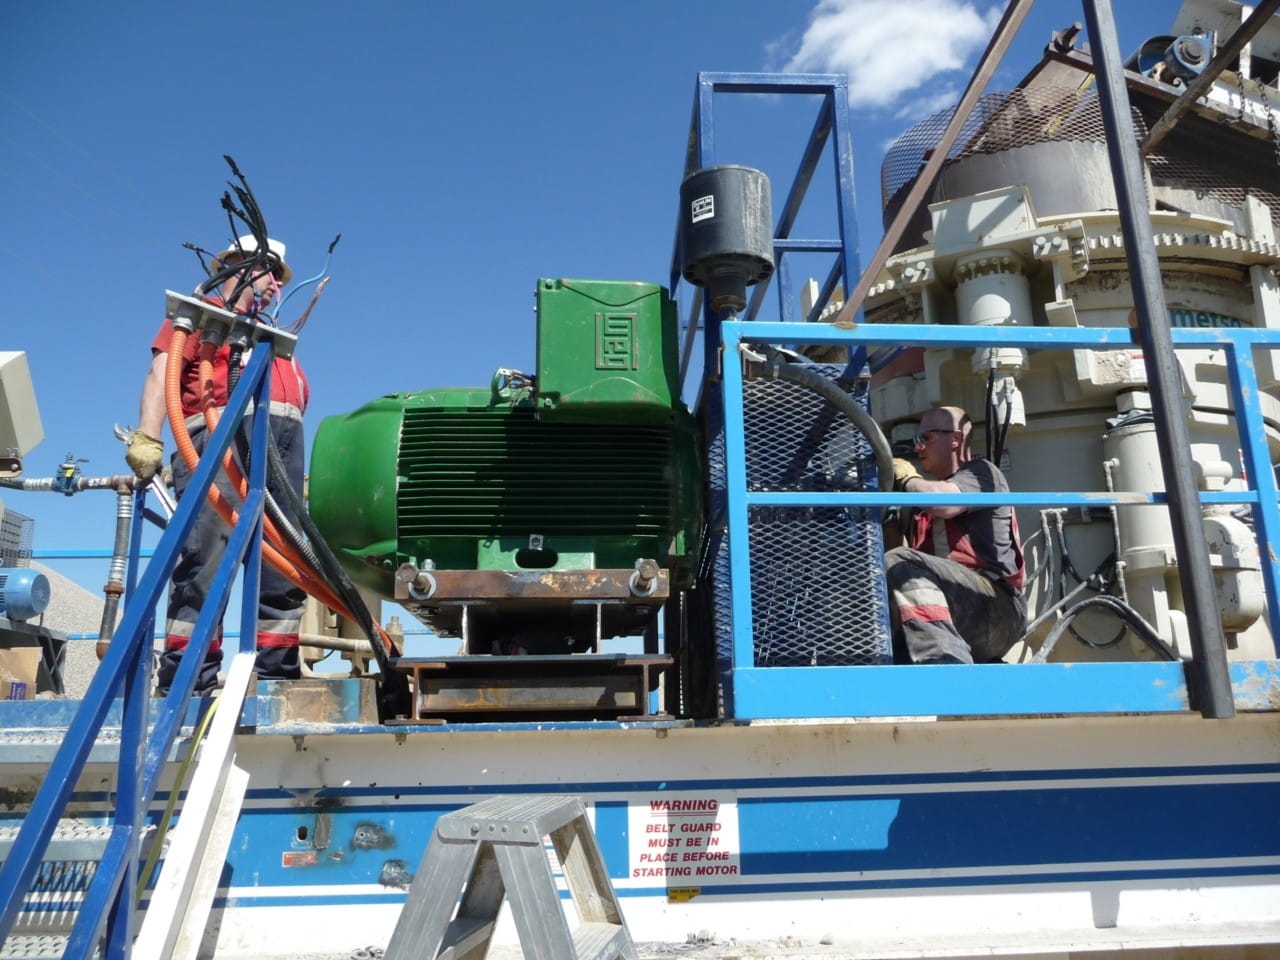
The motor enclosure type that was correct at the time of purchase does not stay correct simply because nobody revisited it. Three common operational events quietly invalidate an earlier ODP decision and none of them typically trigger an electric motor re-spec on their own.
Facility expansion often moves an industrial electric motor from a controlled indoor bay into a space closer to loading docks, outdoor-adjacent bays or newly added processing lines that introduce dust the original layout never had. Process changes. A new material input, a switched cleaning chemical or an added washdown step can introduce moisture or airborne particulate to an area that was previously clean and dry. Relocation, whether the electric motor is moved to a different line during a retrofit or the whole operation shifts to a new site, is the most direct trigger, since the entire premise of the original enclosure selection was built around a location that no longer applies.
The common thread is that none of these changes come with an automatic prompt to revisit motor design decisions made years earlier. That is precisely why enclosure fit needs to be a deliberate checkpoint rather than an assumption carried forward from the original purchase order.
A reactive enclosure fix, meaning a swap made after an industrial electric motor has already failed, is consistently more expensive than the same upgrade made on a planned schedule. Emergency electric motor repairs following an unplanned failure typically run at a significant premium over the same work scheduled in advance, largely because expedited parts, overtime labor and unplanned production loss all stack onto the base repair cost at once.
The production-loss side of that equation is well documented at the industry level. Average unplanned industrial motor downtime cost is in the hundreds of thousands of dollars per hour once lost production, labor and secondary damage are accounted for. The average manufacturing facility loses 27 hours a month to unplanned stoppages. A planned enclosure upgrade, timed to the electric motor's normal replacement cycle or a scheduled maintenance window, avoids nearly all of that premium.
A planned enclosure upgrade, timed to the electric motor's normal replacement cycle or a scheduled maintenance window, avoids nearly all of that premium. The part cost difference between TEFC and ODP at time of purchase is real, but it is a fraction of what an unplanned failure costs once production loss, expedited freight and emergency labor are added to the invoice.
Industrial electric motors paired with a variable frequency drive carry an added reason to get enclosure selection right, because VFD operation changes both the thermal and electrical picture inside the electric motor. Running below rated speed under VFD control reduces the cooling effect an electric motor's own shaft-mounted fan provides, which means an electric motor already running warmer than a fixed-speed application has less thermal margin to absorb the additional stress that airborne contamination inside an ODP enclosure would introduce.
VFDs also introduce induced shaft voltages that can contribute to bearing current damage, a failure mode that compounds rather than competes with contamination-driven bearing wear. An industrial electric motor operating in an ODP enclosure under VFD control is effectively exposed to two separate accelerants on the same component at the same time.
Build enclosure re-evaluation into your standard spec review process rather than treating it as a one-time decision made at initial purchase. Use this checklist whenever an electric motor comes up for replacement, a facility undergoes a layout change or a maintenance record shows a pattern worth investigating:
If two or more of these apply, treat the enclosure decision as open for review rather than settled, even if the motor is still running.
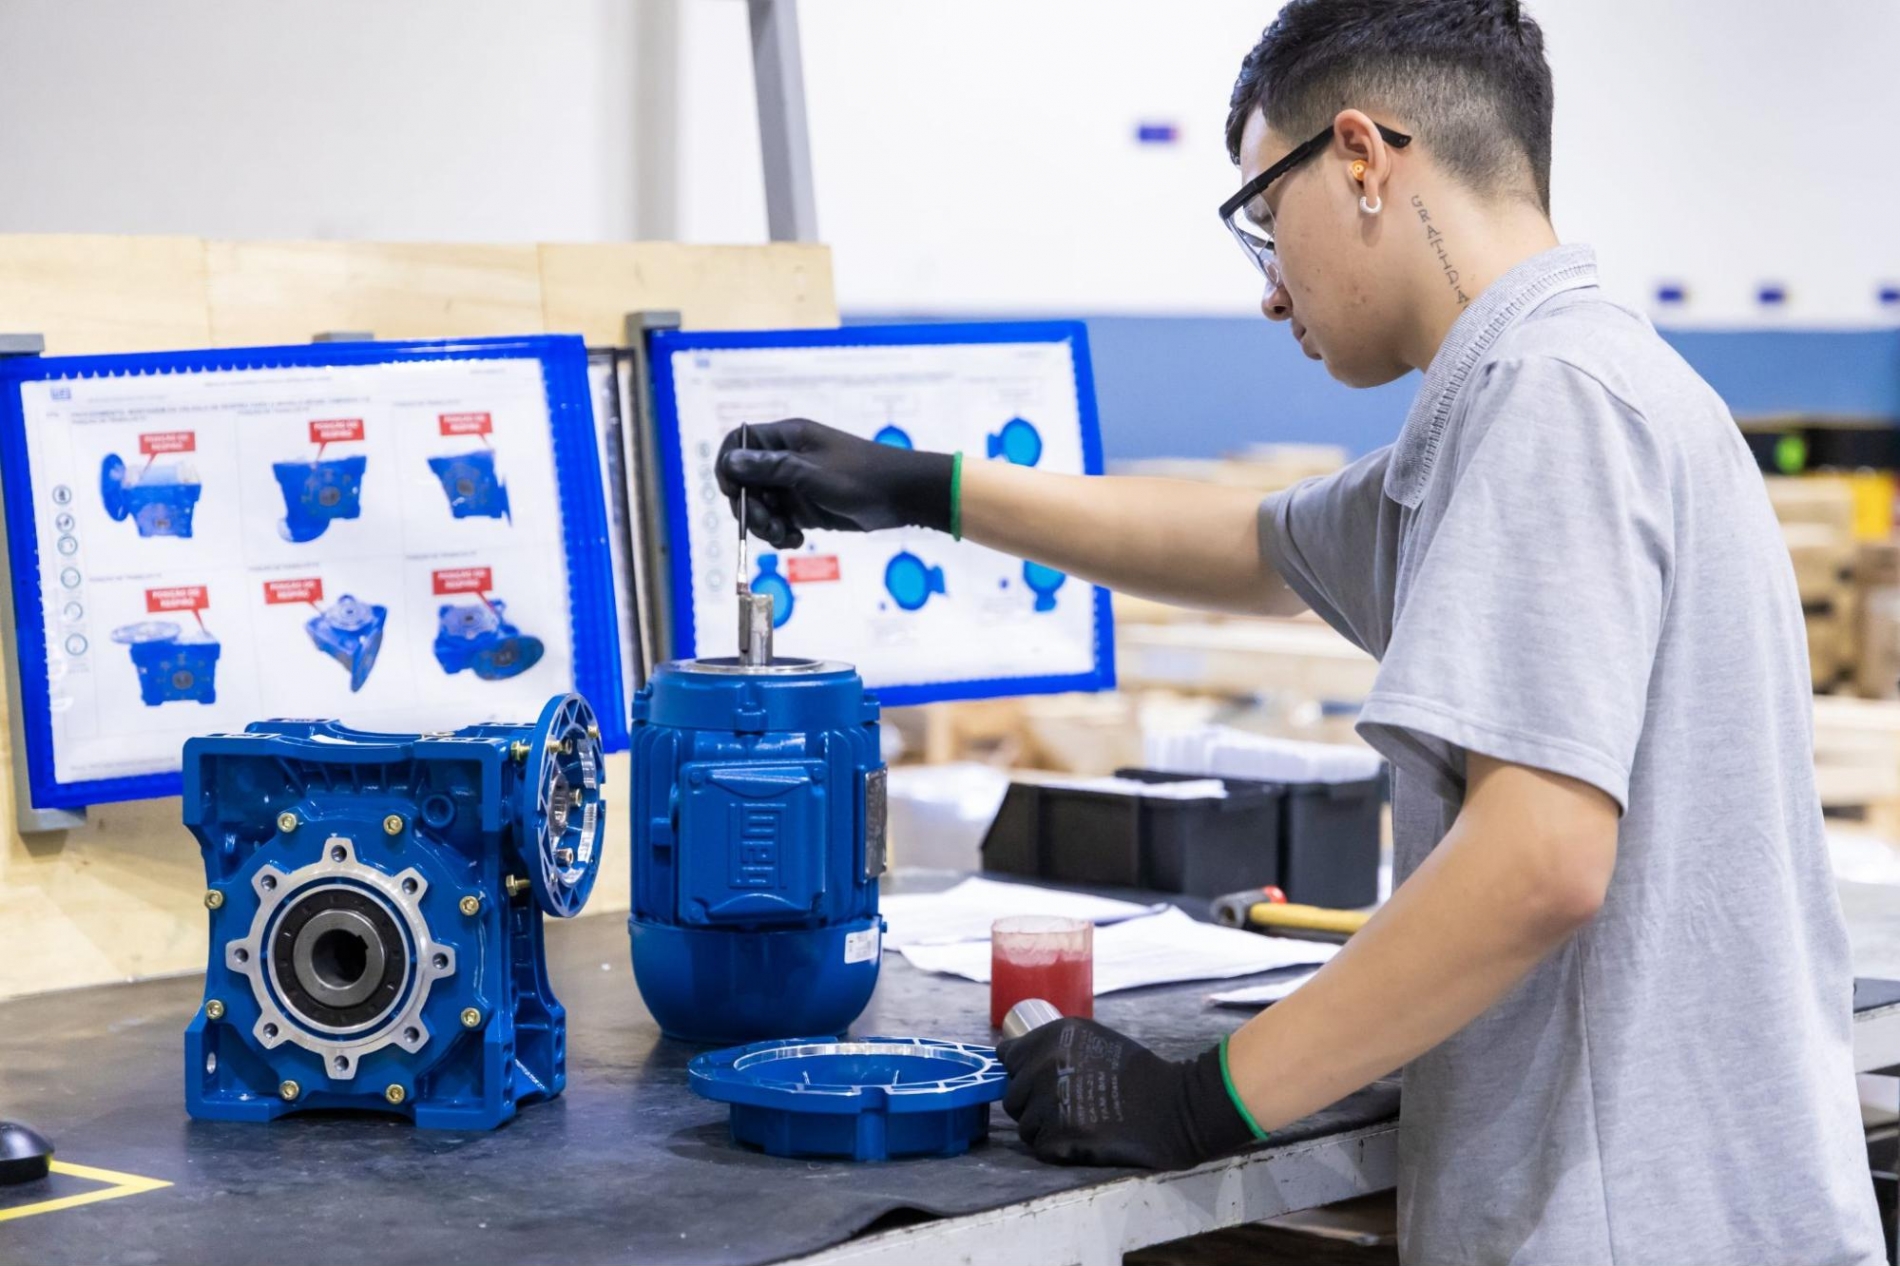
Enclosure mismatch is one of the few electric motor failure risks that is fully within an engineering team's control to catch early, because it does not require new instrumentation or a change in maintenance staffing. It requires comparing the industrial electric motor's original spec against the environment it is actually running in today and building that comparison into the same spec review process used for every other electric motor decision.
If your facility has expanded, your process has changed, or an electric motor class is showing a pattern of early bearing wear, that is the moment to revisit TEFC versus ODP before the next failure decides for you. Contact Pamensky (WEG Canada) today to talk about reviewing your current electric motor fleet against your actual operating conditions and get a straight answer on which units are due for a planned enclosure upgrade at your next replacement cycle.
Reviewed by: Michael Ishlove, Technical Manager
Last reviewed: August 2026
A TEFC (Totally Enclosed Fan Cooled) motor is fully sealed with an external fan providing cooling airflow over the housing, keeping contaminants out of the internal components. An ODP (Open Drip Proof) motor uses open ventilation slots to cool the windings directly with ambient air, which also allows dust and moisture to enter.
Look for a pattern rather than a single symptom: dust or fibre buildup on windings, discoloured or diluted bearing grease, corrosion on the shaft or end brackets and bearing replacement intervals shortening compared to similar motors in cleaner areas of the same facility.
Expansion often moves equipment closer to loading areas, outdoor-adjacent zones or new processing lines that introduce dust or moisture the original location did not have. A motor originally specified for a clean, dry area may now be operating in conditions its enclosure was never rated to handle.
In most cases, yes. A planned upgrade at the next scheduled replacement or maintenance window avoids the expedited parts, overtime labour, and unplanned production loss that come with an emergency swap after failure, at a fraction of the total cost.
Yes. Running below rated speed under VFD control reduces the cooling benefit of a motor's own fan and VFDs can introduce shaft voltages that contribute to bearing current damage. Combined with contamination exposure in an ODP enclosure, this creates two accelerants acting on the same components at once, which is why VJ Pamensky treats VFD pairing as a standing input to enclosure selection.
Any time a motor comes up for replacement, a facility undergoes a layout or process change or maintenance records show a pattern of early bearing or insulation issues. It should be a standing checklist item at spec review, not a one-time decision made only at initial purchase.
Generally, no, not without significant additional protection. ODP motors are designed for clean, dry indoor environments. Outdoor installations, washdown areas and dusty processing environments call for TEFC protection as the standard choice.